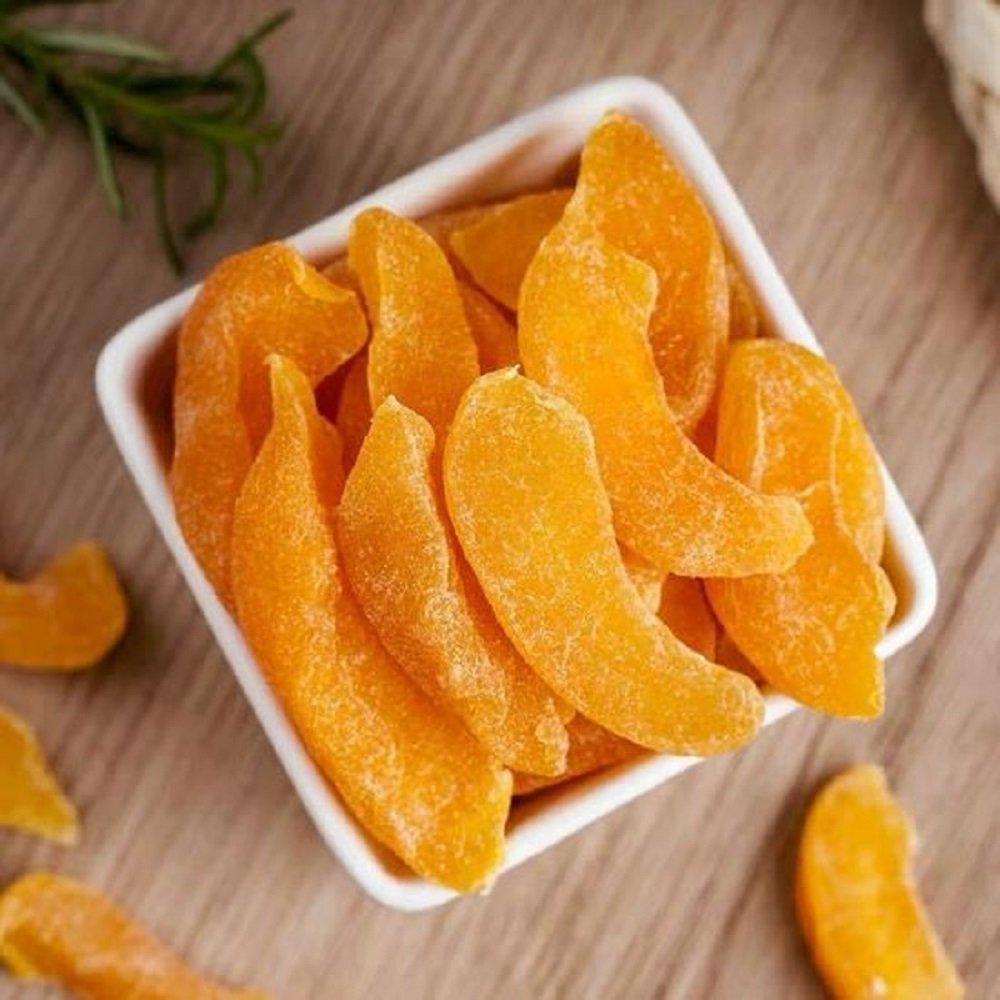
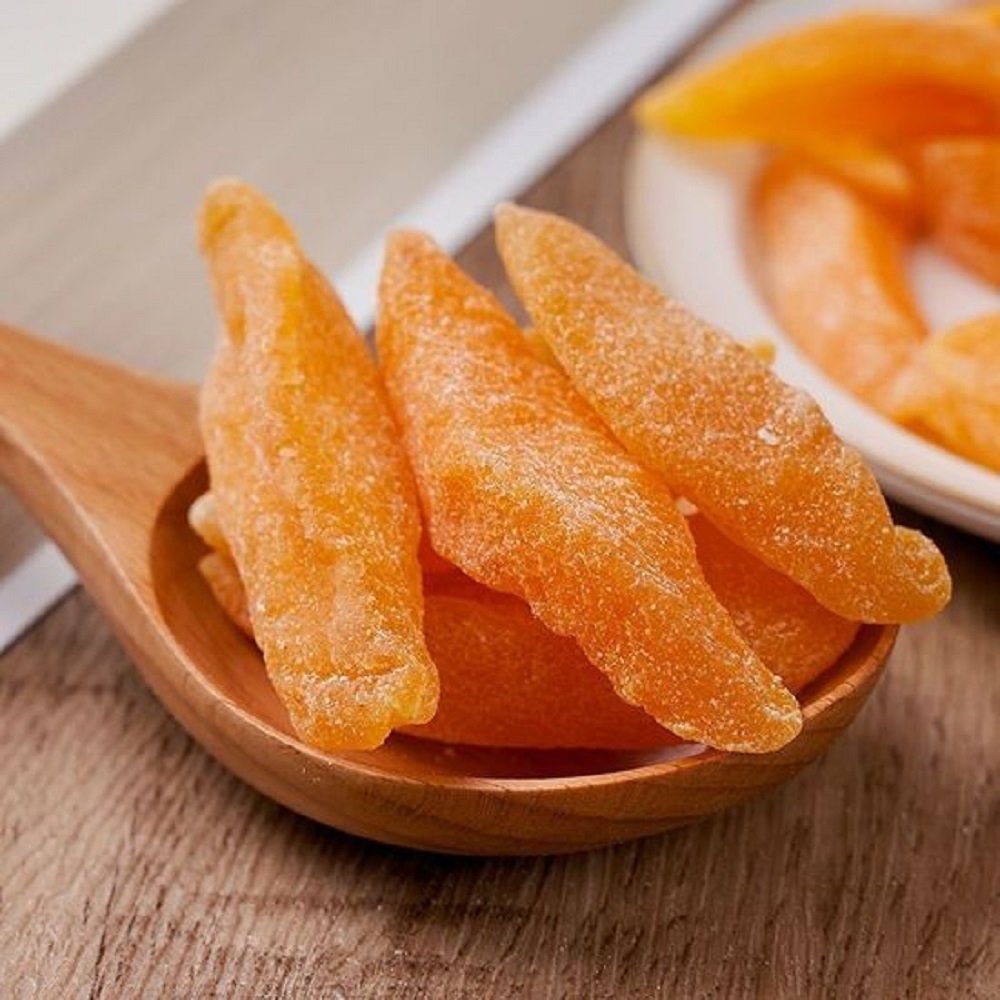
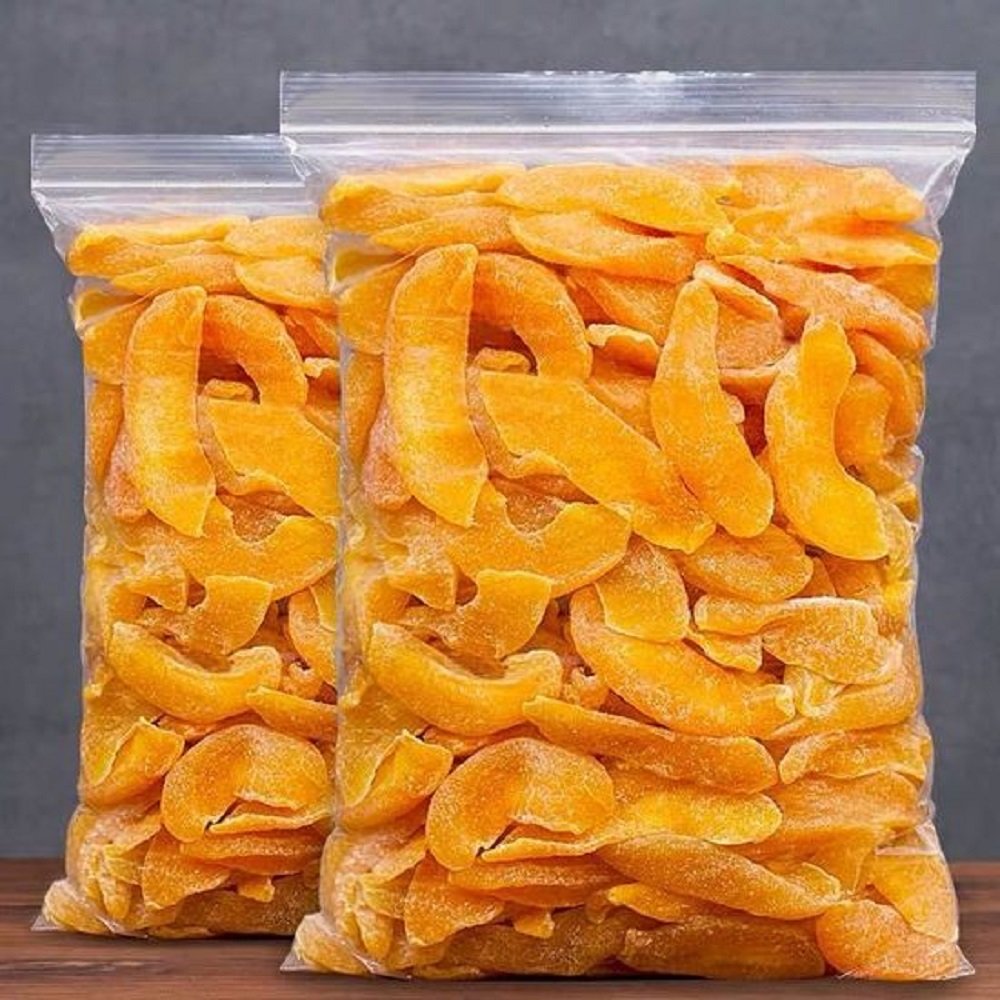
Preserved Yellow Peach Wholesale — Premium Dehydrated Peach Slices & Dices Bulk Supply
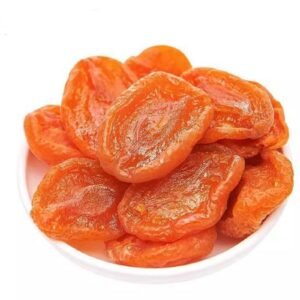
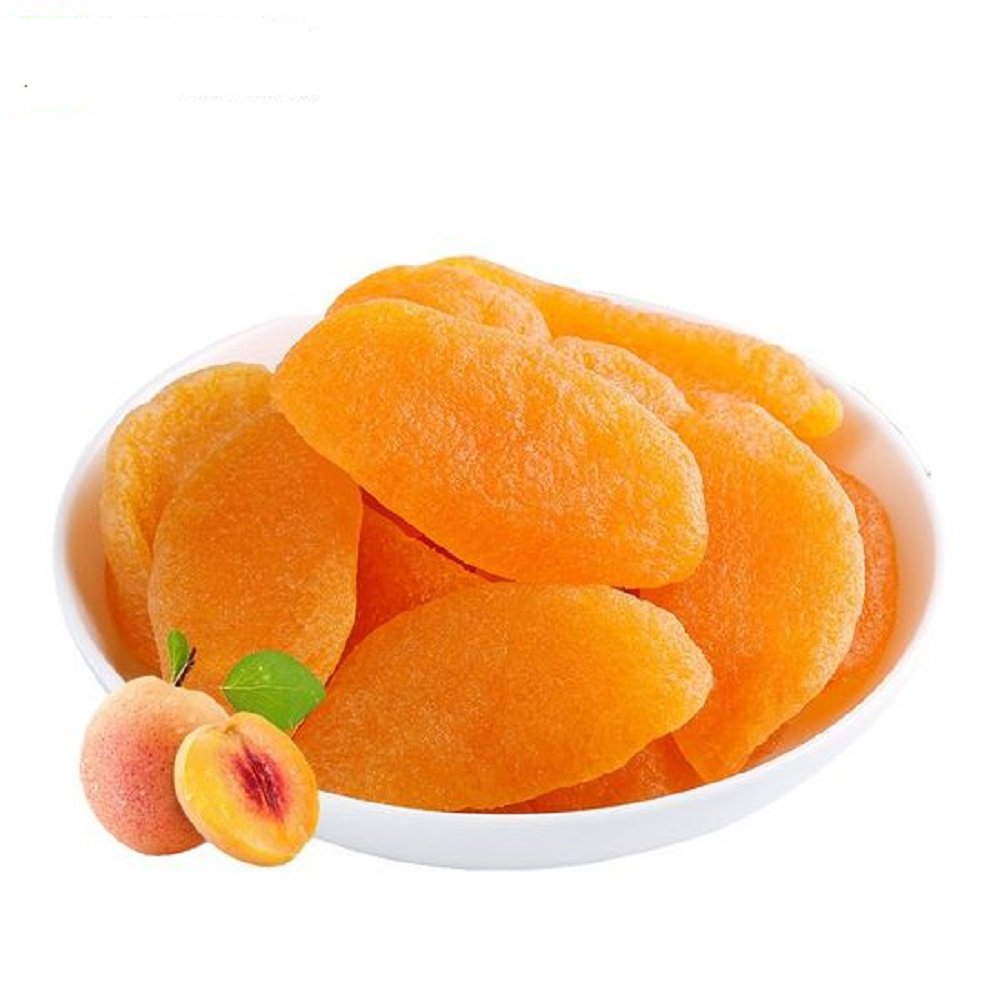
Our industrial Preserved Yellow Peach solutions offer exceptional batch-to-batch consistency and raw material reliability for competitive international food industries. Harvested exactly at the physiological maturity threshold where natural aromatic esters and flesh density peak, the fresh peaches pass through synchronized mechanical washing, peel eradication, and high-precision core evacuation. Through our proprietary controlled osmosis processing coupled with thermodynamics-optimized multi-phase hot air circulation grids, each peach piece retains its characteristic structural cell wall turgor and intense tropical essence, yielding an elite component for complex dry food manufacturing.
Why Global Enterprise Purchasers Specify Our Preserved Yellow Peach
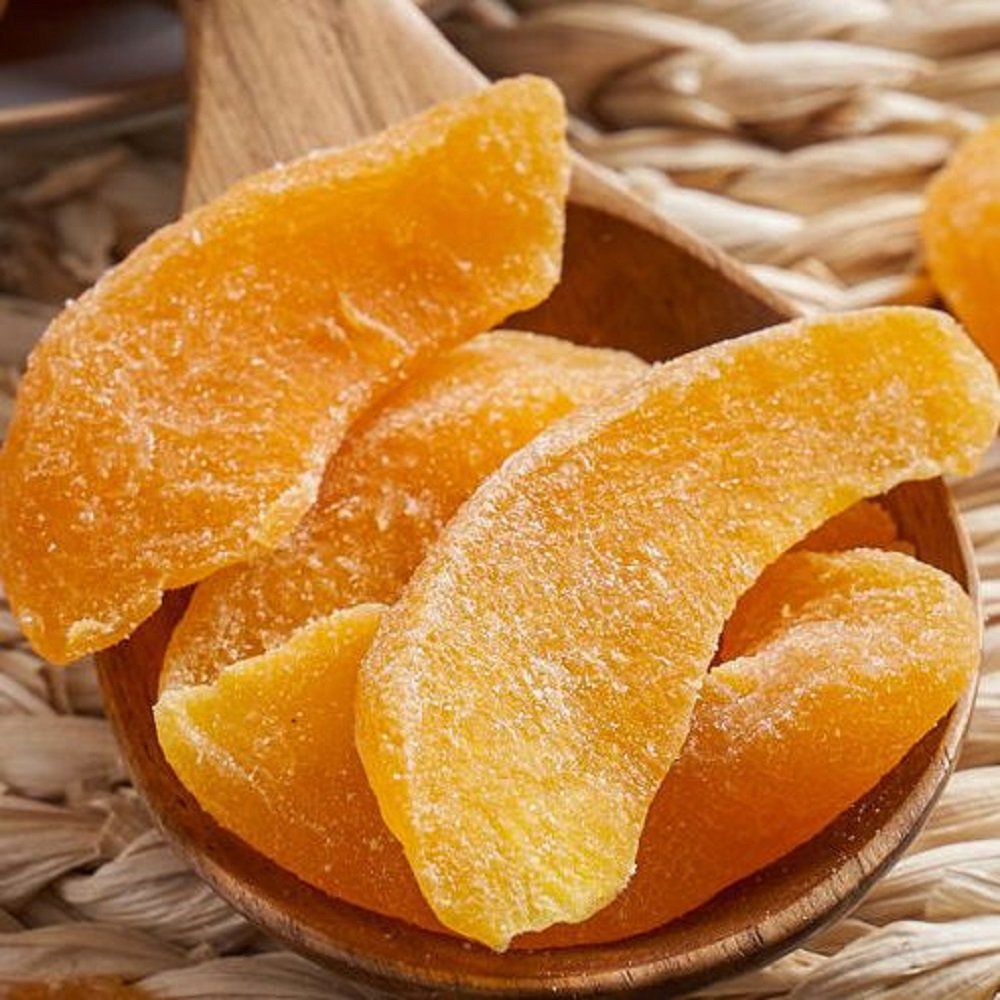
● Superior Golden Hue Retention: Utilizing high-accuracy thermal stabilization curves, we dramatically neutralize polyphenol oxidase systems. This prevents any surface graying or browning, ensuring the final preserved peaches flash an outstanding, clean golden brightness that greatly strengthens retail package aesthetic value.
● Robust Physical Integrity for Processing: The internal free moisture matrix is strictly calibrated to an 18-22% standard baseline. This mechanical balance keeps the peach slices plump and non-collapsing, ensuring they travel cleanly through automated cutting grids or industrial batch hoppers without melting or disintegrating.
● Strict Additive Calibration Protocols: We strictly manage preservative levels depending on your direct country of import. Whether your market dictates an ultra-low sulfur cap (<100 ppm) for European Union compliance, or specific sugar thresholds for low-brix health products, our processing adjustments guarantee hassle-free regulatory cross-border acceptance.
Technical Specifications & Chemical Quality Baseline
| Technical Specifications | Standard Certified Limit | Analytical Methodology / Code |
|---|---|---|
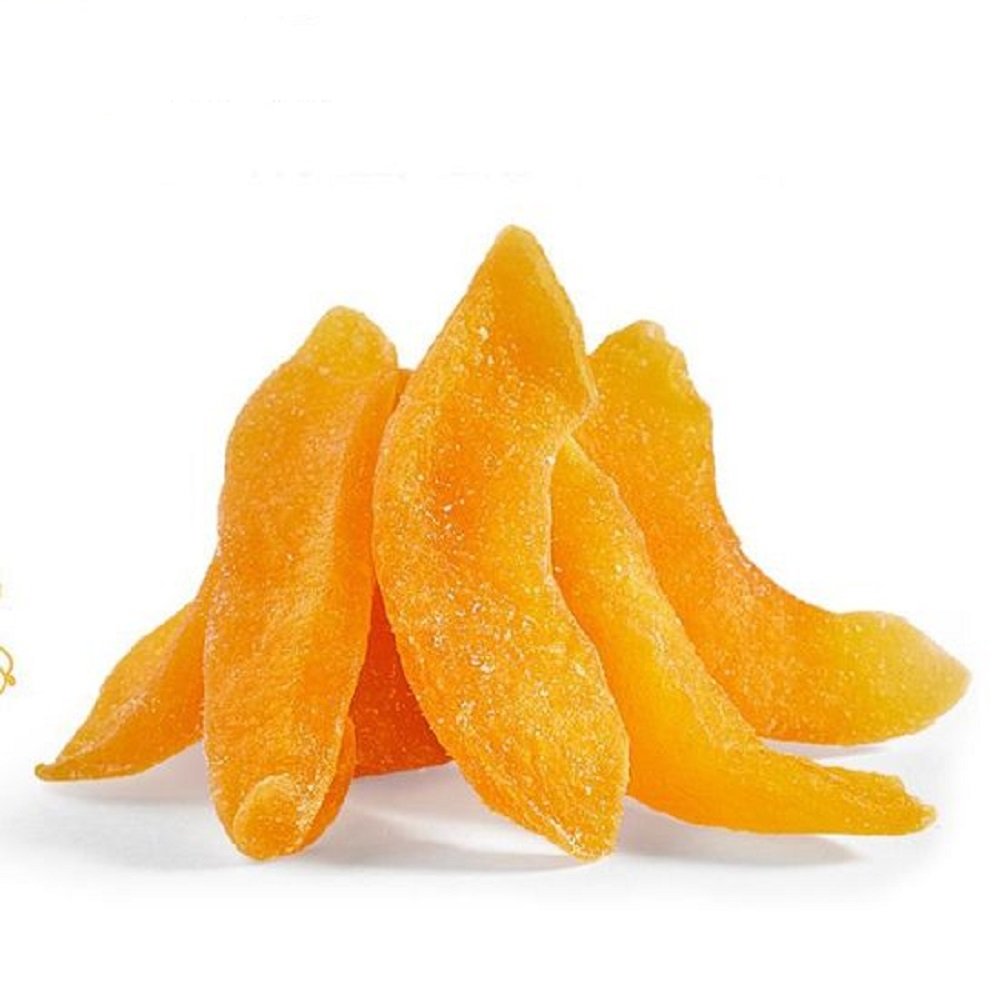
| Organoleptic Criteria | Vibrant bright golden yellow; thick fleshy texture; sweet flavor with intense natural peach aroma | Sensory Panel / Visual Grading |
| Moisture Content | 18% – 22% max | Vacuum Oven Dry Protocol |
| Total Sugar Content | 62% – 68% (Formulation adaptable for lower sugar) | Brix Refractometer Mapping |
| Pit Fragment Residue | Absent / Highly screened (≤ 1 per ton) | Dual-Energy X-Ray Scanning |
| Sulfur Dioxide (SO2) Trace | < 100 ppm for EU compliance | < 500 ppm standard | Optimized Monier-Williams Assay |
| Total Aerobic Count | < 10,000 cfu/g | ISO 4833 Compliance Method |
| Yeast & Mould Colony Count | < 500 cfu/g | ISO 21527 Plate Colony Count |
| Pathogens (E.coli, Salmonella) | Negative in 25g | FDA-BAM Microbiological Codes |
Multi-Sector Commercial Application Profiles
Our wholesale preserved yellow peach slices and dice variants provide crucial aesthetic and functional enhancements across distinct target sectors of the global food manufacturing ecosystem:
- Commercial Cereal, Granola, and Muesli Mixes: Precisely cubed 5mm or 10mm yellow peach pieces inject a lively golden color pop and rich texture contrast alongside dry grains and nuts.
- Industrial Baking, Cakes, and Fruit Panettones: Used widely as non-bleeding inclusions or moisture-stable toppers inside high-temperature oven processes without degrading crumb color profile.
- Premium Snack Blends & Retail Re-bagging: Formatted cleanly into uniform long slices or halves for seamless integration into high-velocity automatic packaging systems for consumer private label lines.
- Dairy, Yogurt, and Ice Cream Preparation: Sized correctly to fit specialized processing fruit preparations, offering distinct tropical bursts that resist freezing solid inside premium ice cream bases.
Supply Chain Stability, Logistical Shielding & Global Dispatch
Bulk intercontinental shipping of sugar-enriched stone fruits calls for uncompromised barrier security. To defeat potential vulnerabilities like sugar sweating, clumping, or premature heat-driven oxidation under changing maritime shipping container temperatures, our factory maintains rigorous logistical protocols. Finished goods are immediately sealed within food-grade, heavy-duty co-extruded double-layer polyethylene inner protective liners before loading into reinforced 5-ply export kraft corrugated master cartons (standardized 10kg arrays). Staged permanently inside climate-mapped departure depots held below 18°C and under 60% relative humidity, our logistics division interfaces with leading global carrier partnerships to assign prioritized, direct ocean shipping slots, maximizing fresh quality arrivals at global distribution hubs.
Frequently Asked Questions (FAQ)
Q1: How does your factory achieve a reliable seed and pit-free standard for bulk yellow peach batches?
A: We implement a specialized triple-stage screening system. Fresh batches undergo mechanical high-velocity alignment and automated pitting coring. Following the dehydration stage, the product stream flows through advanced dual-energy X-Ray inspection grids calibrated to detect dense seed or fragment shadows. Final optical validation by trained quality personnel ensures a nearly flawless, industrial stone-free standard.
Q2: Are we able to request customized cut sizes or lower brix levels for health-food markets?
A: Yes, absolutely. Our high-precision slicing and dicing lines can be reconfigured dynamically to produce custom sizes like 5x5mm, 8x8mm, or tailored strip lengths. We also provide customized low-Brix processing parameters where the total sugar level is tightly scaled back to accommodate clean-label and health-conscious consumer brands.
Q3: What are the best long-term warehousing standards to prevent the peach slices from sticking together?
A: For extended commercial shelf preservation up to 12 months, we mandate keeping bulk containers in dedicated cool storage held below 15°C (ideal conditions range between 4-10°C) with stable relative humidity below 55%. Ensure pallets are kept clear from humid walls and floors to facilitate continuous ambient airflow and prevent pressure block compression.
Q4: What specific food safety and manufacturing certifications accompany your export shipments?
A: Our modern manufacturing plant is verified continuously by international audit bodies. We maintain valid certifications for BRC Global Standard for Food Safety (Grade A status), HACCP tracking systems, and ISO 22000. Additionally, specific output lots are backed by recognized Kosher and Halal compliance certificates to streamline global market entry.